Die Engineering Guides
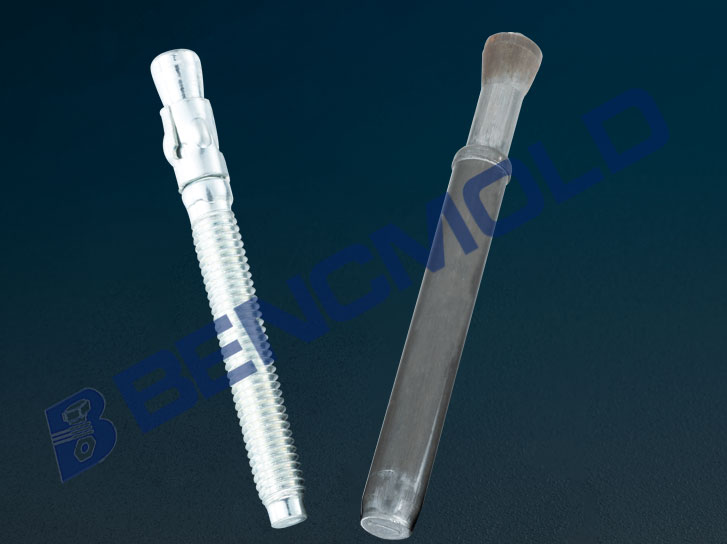
Wedge Anchor Forming with Split Die Tooling – One Shot, No Turning
Wedge anchors formed in one shot by split die tooling on a 134LL multi-station cold former, eliminating taper-end turning and keeping grain flow through the expansion cone.
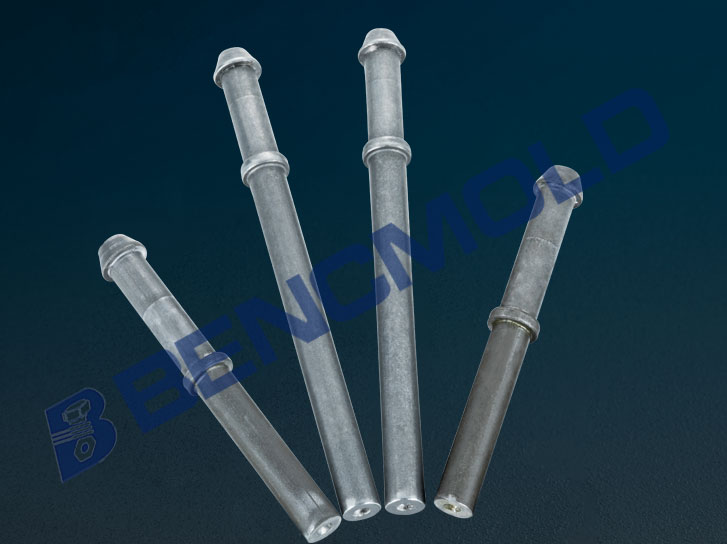
Split Die Cold Forming – Tooling for Parts a Solid Die Cannot Release
Split die cold forming tooling for parts a solid die cannot release - collars, undercuts and overhangs. Two to four segments, patented, in production since 2008.
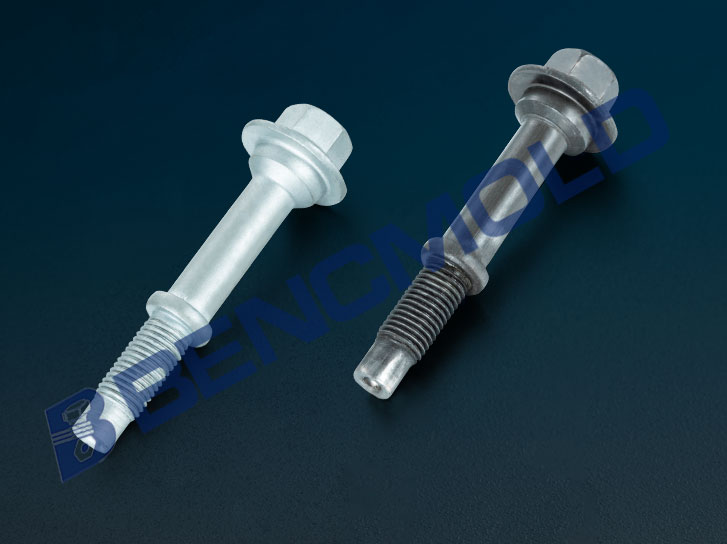
Automotive Muffler Bolts – One-Piece Cold Heading Die, Split Die at Station Four
Automotive muffler bolts formed in one piece in 2008 on a 134L cold heading machine, with a split die at the fourth station - the project that shaped how BENC MOULD develops cold heading dies.
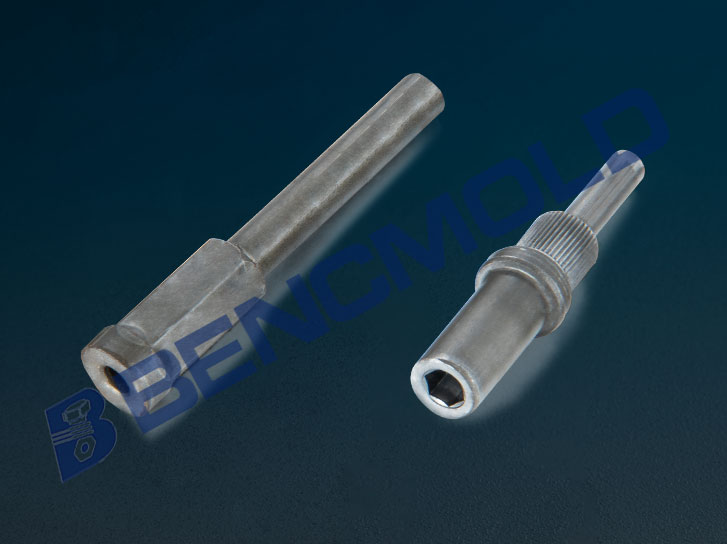
Automotive Non-Standard Fasteners – Custom Cold Heading Die Development
Custom cold heading die development for automotive non-standard fasteners - split dies, special-shaped punch pins and full process development from drawing to stable production.
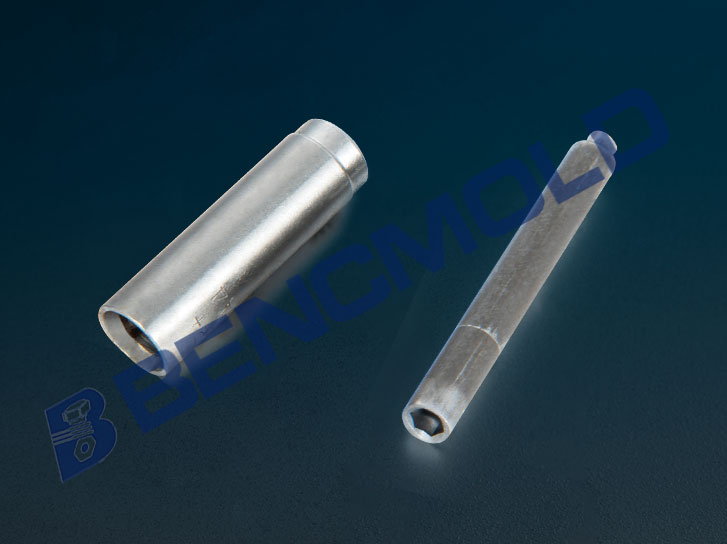
Hollow tube screw
Hollow tube screw One-shot forming using multi-station cold headers (screw cold header 104‑106,134L‑137L,164‑166L or nut cold header), minimizing turning & drilling work. For hollow tube slug ejection, we adopt extruded bright bar (drawn bright bar) process to ensure the inner bore is smooth and free of tear marks.
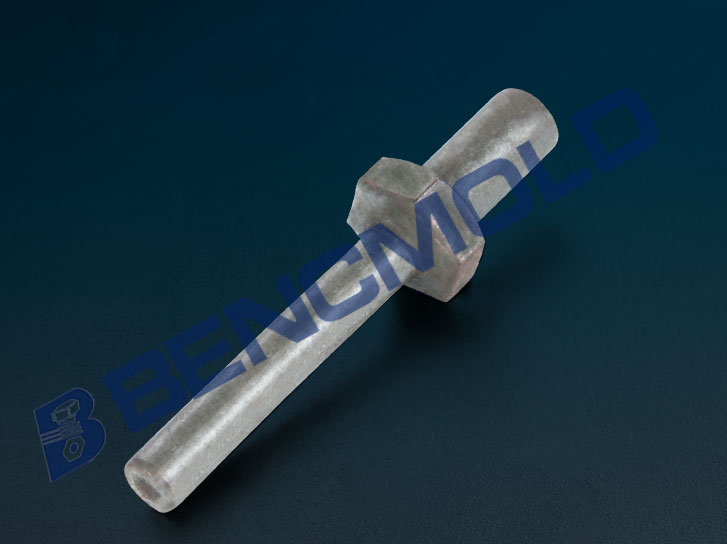
Hex Head Double End Stud
The screw shank is one-shot formed by cold heading machine with double trimming process. The hexagon is burr-free without fracture marks. Pictures are our self-developed actual samples. Contact us for similar products, we offer technical support and communication.
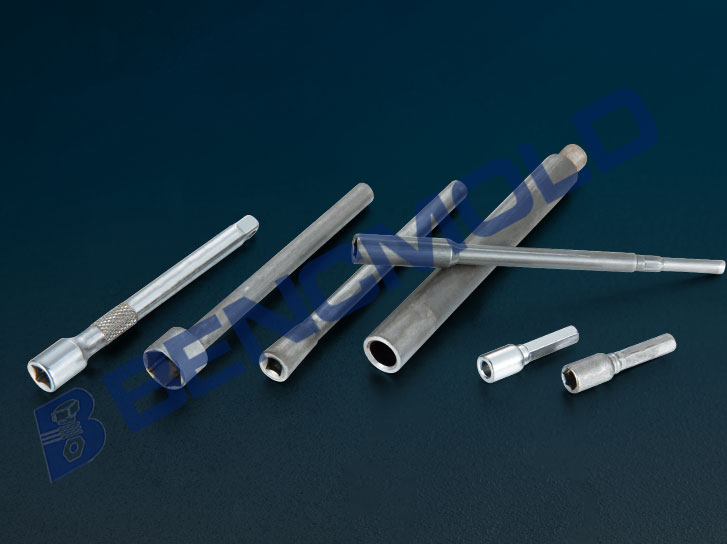
Cold Heading Case of Non-standard Tools
Special-shaped punch pins for electric tool adapter rods — square, hexagonal and Torx punches, CNC ground, one-shot cold heading without die rework.
Cold Heading Die Materials: Carbide vs HSS vs PM Steel
Choosing a cold heading die material is one of the few decisions that locks in everything downstream: hit rate, tolerance drift, regrind interval and scrap rate. Pick too soft and the bore washes out in a week. Pick too hard and the nib chips on the first slug. This guide compares the three families we […]
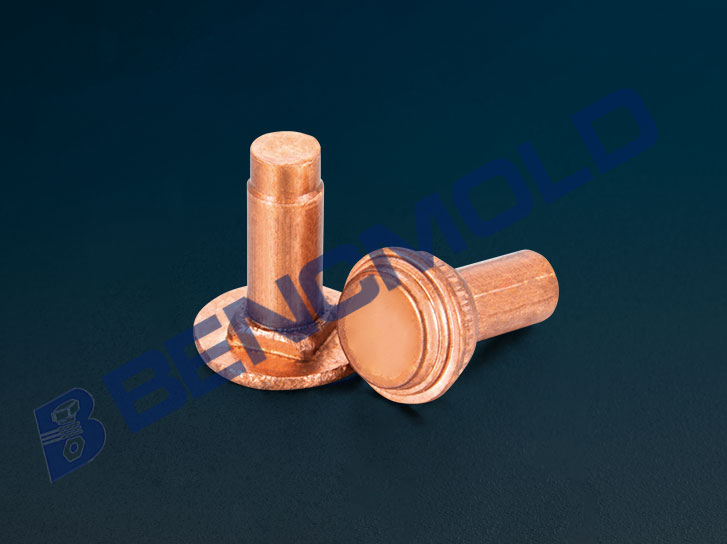
Cold Heading Die Precision: What G4 to G9 Really Means
A die print says G6. Most buyers cannot translate that into what actually arrives in the box, and most suppliers will not explain it, because the honest answer is that the grade number covers only part of what determines whether the part comes out concentric. This page explains what cold heading die precision means in […]
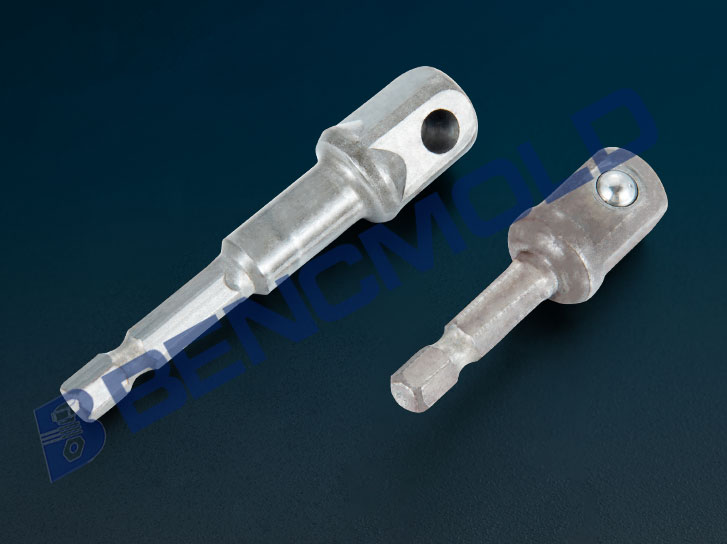
Extrusion Ratio in Cold Heading: Safe Limits and Die Design
The extrusion ratio is the single number that decides whether a shank reduction can be formed in one blow, needs two, or cannot be cold formed at all. It is also the number most often left off the drawing, which is why shank-reduction dies fail in ways that look like material defects but are really […]